Warehouse Handoff
RC Toy 3PL Receiving and Discrepancy Checklist
The first warehouse scan is the moment export cartons become sellable inventory. A clear receiving plan helps distinguish count errors, transport damage and product-quality concerns.
Direct answer: Give the 3PL a SKU-to-carton map and an exception process before arrival, then reconcile the physical receipt against the purchase order and shipping documents. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Sourcing Checklist: What to Confirm Before You Place an Order, RC Toy Quality Control Checklist for B2B Orders, RC Toy Design and Tooling Ownership: Buyer Checklist.
1. Send an advance shipment file
Provide expected SKU, carton count, units per carton, identifiers and appointment details before delivery.
A driver arriving with unlabeled mixed pallets leaves the warehouse guessing. The advance file should identify the shipment reference, container or tracking number, gross count and any mixed-case rules. Where the receiving system supports it, map retail and case identifiers separately. Correct the file if the factory changes final packed quantities after pre-shipment inspection.
During factory testing and shipment preparation, use send an advance shipment file as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Inspect the exterior first
Record crushed, wet, torn or resealed cartons before they are moved into ordinary stock.
The receiver should photograph labels, pallet condition and damage at the point of handoff. This does not prove what caused the damage, but it preserves evidence for a later carrier discussion. Create a quarantine location for affected cases so they are not sold while an importer and insurer decide whether to open or sample them.
During factory testing and shipment preparation, use inspect the exterior first as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Scan and count by hierarchy
Compare pallet, case and each-level data using the identifiers agreed in the item master.
A case labeled as twelve units but containing ten can produce an invisible shortage if receiving counts only outer cartons. For mixed cartons, the 3PL needs a line-level packing list and a way to record exceptions by SKU. Barcode failure should be captured as an operational defect, not silently bypassed by typing an approximate item number.
During factory testing and shipment preparation, use scan and count by hierarchy as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Sample the contents with a defined rule
Set a targeted opening plan for damage, count or identity verification without turning receiving into a full product laboratory.
The warehouse can check whether the vehicle, controller, cable and manual are visibly present, while a qualified quality team handles functional or safety testing. Define who authorizes opening and how the case is resealed. If many cartons show the same issue, escalate the sampling plan instead of assuming that one clean box represents the entire shipment.
During factory testing and shipment preparation, use sample the contents with a defined rule as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Classify discrepancies
Separate shortage, overage, wrong SKU, carton damage, barcode error and suspected product defect.
These categories have different owners and remedies. An overage of a wrong color is not the same as a missing case. Write the observed fact, count and evidence reference, then compare with factory packing records and carrier documentation. Avoid blaming a party before the handoff records are reviewed. A consistent taxonomy also improves future supplier and freight reviews.
During factory testing and shipment preparation, use classify discrepancies as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Release inventory in stages
Make only accepted stock available to sales while exceptions are investigated.
A retailer may have a promotion scheduled, so a blanket hold can be expensive; releasing damaged or unidentified goods is also risky. Set release criteria for clean cartons, and keep suspect cases on hold with a visible status. The importer should own the decision on rework, repack, credit or claim submission, informed by the 3PL photographs and counts.
During factory testing and shipment preparation, use release inventory in stages as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Close the feedback loop
Return a concise receipt report to the factory, forwarder and commercial team.
The report should state received quantities by SKU, discrepancies, photographs, immediate containment and a requested response date. Compare receiving issues with the pre-shipment inspection and carton design. A repeated corner crush may call for packaging change, while recurring wrong labels may require a packing-line control. Use the learning on the next purchase order.
During factory testing and shipment preparation, use close the feedback loop as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
Suppose a distributor expects 240 cartons of two RC vehicle models. The 3PL counts 240 outer cases and initially marks the shipment complete. Later, order picking shows that twenty cases labeled as model A contain model B. The physical carton total was correct, but SKU inventory and retailer commitments were not. A better receiving plan requires the advance file to list each case identifier and the units inside; a targeted case-opening check should include mixed or suspicious pallets. The receiver records the carton marks, photographs the contents and quarantines the mismatched cases while clean stock is released. The importer compares this evidence with the supplier packing list and pre-shipment report, then decides whether relabeling is permitted or replacement stock is needed. The 3PL should not silently edit inventory to make totals balance. A precise discrepancy report gives the factory a chance to correct the packing-line control for the next order.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see GS1 Global Data Model: Official guidance on standardized product attributes used to list, order, store and sell products.
Photography plan for this article
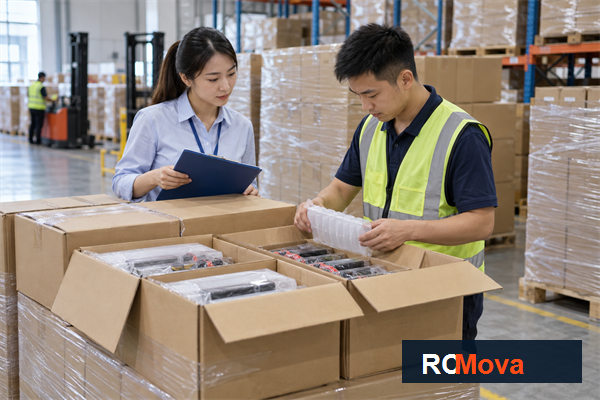
Article hero image — After the opening section
Image title: RC Toy 3PL Receiving and Discrepancy Checklist — RC toy sourcing overview
Caption: Battery-related shipment planning should be checked against the actual product and packing configuration. Article focus: rc toy 3pl receiving.
ALT text: Asian logistics staff checking packed RC toy export cartons in a Shenzhen warehouse; rc toy 3pl receiving buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy 3PL Receiving and Discrepancy Checklist, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
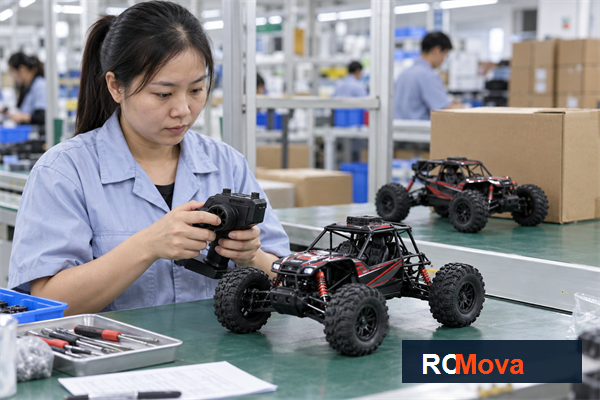
In-article supporting image — Before the FAQ section
Image title: RC Toy 3PL Receiving and Discrepancy Checklist — RC toy quality and shipment check
Caption: Production review for rc toy 3pl receiving before the export handoff.
ALT text: Asian quality team reviewing rc toy 3pl receiving with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy 3pl receiving against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about send an advance shipment file?
Provide expected SKU, carton count, units per carton, identifiers and appointment details before delivery. A driver arriving with unlabeled mixed pallets leaves the warehouse guessing. The advance file should identify the shipment reference, container or tracking number, gross count and any mixed-case rules. Where the receiving system supports it, map retail and case identifiers separately. Correct the file if the factory changes final packed quantities after pre-shipment inspection.
How should buyers verify sample the contents with a defined rule?
Set a targeted opening plan for damage, count or identity verification without turning receiving into a full product laboratory. The warehouse can check whether the vehicle, controller, cable and manual are visibly present, while a qualified quality team handles functional or safety testing. Define who authorizes opening and how the case is resealed. If many cartons show the same issue, escalate the sampling plan instead of assuming that one clean box represents the entire shipment.
What should be confirmed before shipment?
Return a concise receipt report to the factory, forwarder and commercial team. The report should state received quantities by SKU, discrepancies, photographs, immediate containment and a requested response date. Compare receiving issues with the pre-shipment inspection and carton design. A repeated corner crush may call for packaging change, while recurring wrong labels may require a packing-line control. Use the learning on the next purchase order.
Conclusion: turn the decision into a working plan
Give the 3PL a SKU-to-carton map and an exception process before arrival, then reconcile the physical receipt against the purchase order and shipping documents. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements