Electronics Quality
RC Toy PCB and Solder Quality: Buyer Checks
Electronics workmanship is a reliability input, not an optional detail hidden inside the shell. Buyers should connect PCB acceptance to the actual toy failure modes they observe.
Direct answer: Specify the applicable assembly standard and product-specific checkpoints, then review soldered joints, connectors and finished-vehicle function on representative units. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Quality Inspection and Defect Checks: Buyer Guide, RC Toy Quality Control Checklist for B2B Orders, What Should Buyers Check for Quality Comparison When Sourcing Remote Control Toys?.
1. Map the electrical path
Identify the board, motor wires, switch, charging connection, battery leads and controller interface.
A useful inspection plan follows likely stress points rather than asking someone to look at every component equally. A wire that flexes when the battery door opens may need strain relief, while a fixed PCB connection may need visual workmanship checks. The exact product layout determines which areas are critical.
During factory testing and shipment preparation, use map the electrical path as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Agree a workmanship reference
Use a current relevant electronics assembly standard and a product-specific acceptance addendum.
IPC-A-610 is a recognized reference for electronic assembly acceptability, but saying IPC compliant on a quote is not enough. Specify the revision, applicable class or contractual criteria with a qualified electronics engineer. Do not imply that an external certification automatically covers the entire RC toy. The board must still meet the finished product’s mechanical and electrical needs.
During factory testing and shipment preparation, use agree a workmanship reference as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Inspect wires and connectors
Check solder wetting, exposed conductors, connector retention, polarity and routing near moving parts.
A strong solder joint can still be compromised by a cable pulled tight across the chassis. Assess how assembly workers place and secure leads, especially near wheels, gears and battery doors. Use photographs of acceptable routing and a simple pull or flex check where engineering has defined it. Avoid inventing force thresholds without product validation.
During factory testing and shipment preparation, use inspect wires and connectors as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Look for process consistency
Ask for first-article checks, operator training records and a response to recurring defects.
One neat demonstration board does not represent thousands of toys. Sampling across shifts or lots can show whether the workmanship stays consistent. If the same intermittent steering complaint appears repeatedly, correlate it with board supplier, solder process and vehicle lot before attributing every return to consumer misuse.
During factory testing and shipment preparation, use look for process consistency as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Pair visual checks with function tests
Power and drive the finished product after assembly, including a repeatable steering and charging routine.
Visual inspection can detect poor joints, but not every electrical problem is visible. A function test verifies the integrated system while a board-level check helps explain a failure. Define the time, sequence and pass condition so different operators do not perform different informal tests under the same checklist heading.
During factory testing and shipment preparation, use pair visual checks with function tests as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Control rework and substitutions
Document any board repair, replacement component or alternate solder process that enters production.
Reworked boards can be acceptable when a qualified process and inspection are defined, but they should not disappear into normal stock without traceability. A changed switch or connector can alter fit or user feel. Keep approval records with the lot and decide whether the change affects previous test evidence or spare-parts compatibility.
During factory testing and shipment preparation, use control rework and substitutions as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Use field evidence carefully
Feed no-power and intermittent-control returns into a controlled failure analysis.
The return reason written by a retailer is a starting clue, not a root cause. Inspect the battery, charging method, controller pairing and PCB connection before deciding what failed. Share anonymized failure patterns with the electronics supplier and verify any correction in production units. This closes the loop between warehouse complaints and factory controls.
During factory testing and shipment preparation, use use field evidence carefully as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
Suppose a retailer reports RC cars that run correctly for a few minutes and then intermittently lose steering. Returned units are inspected with the battery and controller first so a setup issue is not mistaken for a board defect. Several units show a loose connection at the steering motor lead after mild chassis movement. The factory reviews the solder workmanship, cable routing and strain relief on the affected lot, using the agreed assembly acceptance criteria. A corrective action may include a routing change and a revised inspection checkpoint, followed by representative finished-vehicle tests. The buyer asks whether earlier stock needs additional screening and whether the correction changes spare-part compatibility. The lesson is not that every intermittent fault is a solder problem; it is that a repeatable failure analysis can turn a vague return category into a specific, verifiable production control.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see IPC document revision table: Official listing of electronics assembly and inspection standards, including IPC-A-610.
Photography plan for this article
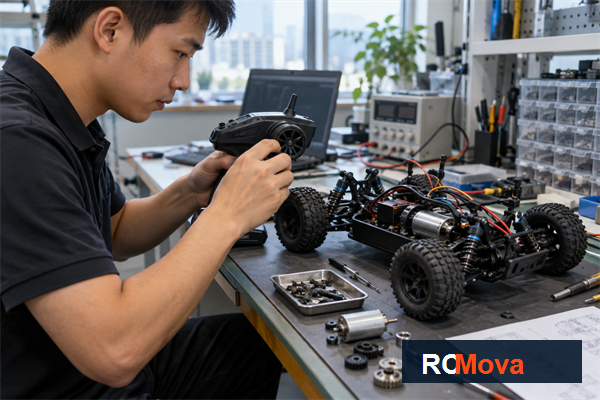
Article hero image — After the opening section
Image title: RC Toy PCB and Solder Quality: Buyer Checks — RC toy sourcing overview
Caption: Controller selection should be tested as part of the complete vehicle and user experience. Article focus: rc toy pcb inspection.
ALT text: Asian electronics technician testing an RC controller and vehicle components; rc toy pcb inspection buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy PCB and Solder Quality: Buyer Checks, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
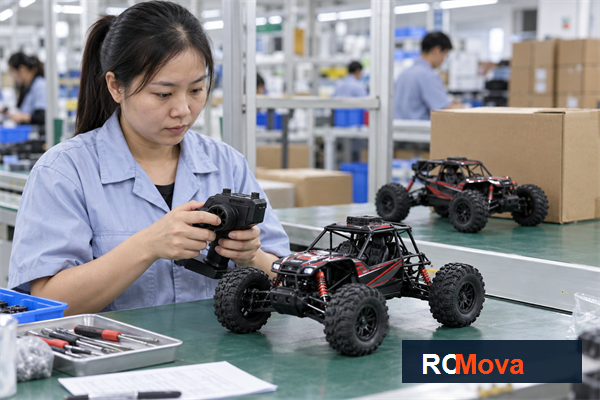
Image title: RC Toy PCB and Solder Quality: Buyer Checks — RC toy quality and shipment check
Caption: Production review for rc toy pcb inspection before the export handoff.
ALT text: Asian quality team reviewing rc toy pcb inspection with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy pcb inspection against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about map the electrical path?
Identify the board, motor wires, switch, charging connection, battery leads and controller interface. A useful inspection plan follows likely stress points rather than asking someone to look at every component equally. A wire that flexes when the battery door opens may need strain relief, while a fixed PCB connection may need visual workmanship checks. The exact product layout determines which areas are critical.
How should buyers verify look for process consistency?
Ask for first-article checks, operator training records and a response to recurring defects. One neat demonstration board does not represent thousands of toys. Sampling across shifts or lots can show whether the workmanship stays consistent. If the same intermittent steering complaint appears repeatedly, correlate it with board supplier, solder process and vehicle lot before attributing every return to consumer misuse.
What should be confirmed before shipment?
Feed no-power and intermittent-control returns into a controlled failure analysis. The return reason written by a retailer is a starting clue, not a root cause. Inspect the battery, charging method, controller pairing and PCB connection before deciding what failed. Share anonymized failure patterns with the electronics supplier and verify any correction in production units. This closes the loop between warehouse complaints and factory controls.
Conclusion: turn the decision into a working plan
Specify the applicable assembly standard and product-specific checkpoints, then review soldered joints, connectors and finished-vehicle function on representative units. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements