Process Performance
RC Toy Production Yield and Rework: Buyer Review
Yield data shows how consistently the production process creates acceptable RC toys before repair or sorting. It should be interpreted with defect definitions and lot context, not used as an isolated supplier score.
Direct answer: Review first-pass yield, rework and scrap by process and defect type, then verify that corrective actions protect the released shipment and future orders. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Importers want to understand whether production problems are being contained and corrected rather than hidden by final sorting. A shipment can pass a final sample while high internal rework signals unstable processes, mixed components or schedule pressure.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see How to Evaluate an RC Toy Sample Before Mass Production, RC Toy Production Lead Time: How to Plan a More Reliable Launch, RC Toy OEM Projects: A Buyer Guide From Brief to Production.
1. Agree the yield definitions
Define first-pass acceptance, rework, repair, scrap and retest consistently before comparing numbers.
A unit adjusted during normal assembly may not be classified the same way as a completed unit returned from final test. Ask the supplier to explain the boundary. Do not compare two factories unless they count at similar process stages. The useful objective is a stable internal trend that connects a loss category with the operation and product version responsible.
During factory testing and shipment preparation, use agree the yield definitions as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Separate data by process and SKU
A total factory percentage can hide a severe problem on one model, color or production step.
Review molding, decoration, electronics, assembly, testing and packing losses at an appropriate level. Mixed-SKU orders should show the affected model. A new body shell may have cosmetic scrap while the shared chassis remains stable. Keep the analysis proportional to risk and order value; buyers need meaningful visibility, not every confidential production statistic.
During factory testing and shipment preparation, use separate data by process and sku as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Prioritize repeat defects
Rank issues by frequency, severity, customer impact and likelihood of escaping the factory.
A frequent cosmetic touch-up and an intermittent loss of control require different responses. Use a simple Pareto view or ranked list with counts, not only percentages. Confirm whether the defect was found at the creating process or much later. Late detection increases rework and may indicate that an earlier check or fixture should be improved.
During factory testing and shipment preparation, use prioritize repeat defects as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Control rework instructions
Reworked units need an approved method, trained operator and defined retest before packing.
Informal repair can introduce stripped screws, damaged wires or mixed components. Identify what may be reworked and what must be scrapped or escalated. Record affected quantities and the person authorizing the method. After rework, repeat the functions and visual checks that could have been disturbed rather than testing only the original symptom.
During factory testing and shipment preparation, use control rework instructions as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Protect lot identity
Keep rejected, reworked and accepted units physically and digitally separated through disposition.
Use labeled areas or containers so unverified products do not flow back to packing. When a component batch drives the issue, maintain traceability to affected finished units. If acceptable units are sorted from a suspect group, document the screening criterion and coverage. A sorting action contains risk for the current lot but does not by itself correct the process.
During factory testing and shipment preparation, use protect lot identity as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Verify corrective action
Require evidence that the cause and control changed, not merely that the final quantity was recovered.
Evidence may include a revised fixture, incoming check, work instruction, supplier action or setup parameter. Review several consecutive units after implementation and monitor whether the defect recurs. Avoid claiming statistical capability from a small sample. For safety-relevant or regulatory issues, involve qualified technical and compliance personnel before release.
During factory testing and shipment preparation, use verify corrective action as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Use trends for the next order
Carry open risks and verified improvements into pre-production planning for reorders.
Compare the next run using the same definitions and similar configuration. A lower defect count after a material change is encouraging, but volume and inspection coverage matter. Share a concise buyer report that explains major issues, containment and prevention without turning internal yield into an unsupported product-quality guarantee.
During factory testing and shipment preparation, use use trends for the next order as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A factory reports that all packed units passed final function testing, yet the order finished several days late. The buyer asks for a high-level defect trend and learns that many vehicles required steering linkage adjustment after assembly. The team traces the pattern to a component tolerance stack and changes the incoming gauge and assembly fixture. Repaired units receive the full function routine again and are identified in the rework record. In this illustrative buyer scenario, the shipment decision still relies on finished-product inspection, while yield data reveals the process problem that sorting alone would leave for the next order.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
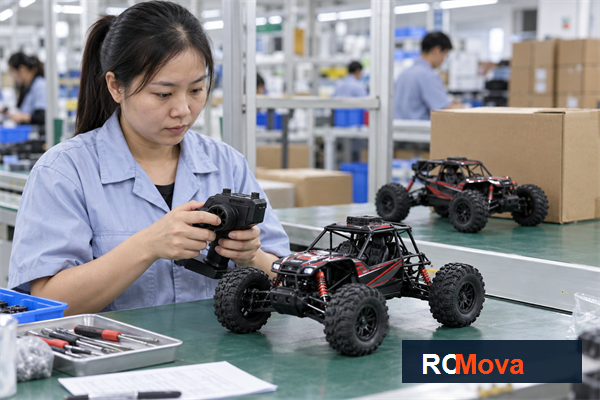
Article hero image — After the opening section
Image title: RC Toy Production Yield and Rework: Buyer Review — RC toy sourcing overview
Caption: Function checks and inspection records help keep an approved configuration consistent before packing. Article focus: rc toy production yield.
ALT text: Asian quality inspector testing an RC vehicle at a Shenzhen factory inspection bench; rc toy production yield buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Production Yield and Rework: Buyer Review, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
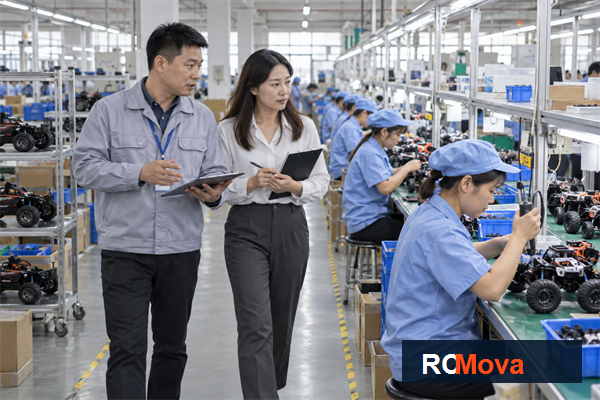
In-article supporting image — Before the FAQ section
Image title: RC Toy Production Yield and Rework: Buyer Review — RC toy quality and shipment check
Caption: Production review for rc toy production yield before the export handoff.
ALT text: Asian quality team reviewing rc toy production yield with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy production yield against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about agree the yield definitions?
Define first-pass acceptance, rework, repair, scrap and retest consistently before comparing numbers. A unit adjusted during normal assembly may not be classified the same way as a completed unit returned from final test. Ask the supplier to explain the boundary. Do not compare two factories unless they count at similar process stages. The useful objective is a stable internal trend that connects a loss category with the operation and product version responsible.
How should buyers verify control rework instructions?
Reworked units need an approved method, trained operator and defined retest before packing. Informal repair can introduce stripped screws, damaged wires or mixed components. Identify what may be reworked and what must be scrapped or escalated. Record affected quantities and the person authorizing the method. After rework, repeat the functions and visual checks that could have been disturbed rather than testing only the original symptom.
What should be confirmed before shipment?
Carry open risks and verified improvements into pre-production planning for reorders. Compare the next run using the same definitions and similar configuration. A lower defect count after a material change is encouraging, but volume and inspection coverage matter. Share a concise buyer report that explains major issues, containment and prevention without turning internal yield into an unsupported product-quality guarantee.
Conclusion: turn the decision into a working plan
Review first-pass yield, rework and scrap by process and defect type, then verify that corrective actions protect the released shipment and future orders. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements