Retail Loss Prevention
Tamper-Evident RC Toy Packaging for Retail
Retail package security should protect a complete RC toy set without making legitimate opening difficult or obscuring mandatory information.
Direct answer: Map what can be removed at the shelf, select visible opening evidence and test the pack with both store staff and shoppers before bulk production. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Car vs. RC Truck: How Retail Buyers Choose the Right Category, Custom RC Toy Packaging Guide for Private-Label Buyers, How to Source RC Construction Toys for Retail and Private Label.
1. Identify the missing-item risk
List the controller, battery pack, charging cable, manual and detachable accessories in the retail box.
A vehicle may remain on display while a small charger disappears. Review which items can be reached through windows or gaps and which are hidden in a secondary compartment. Use retailer shrink and return data if available, but do not assume every missing accessory is theft; packing errors can look the same at the customer-service desk.
During factory testing and shipment preparation, use identify the missing-item risk as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Define visible opening evidence
Choose seals or structural closures that show ordinary access without claiming perfect tamper prevention.
A sticker that lifts cleanly and reseals may offer little useful evidence. A destructible label, patterned tape or tear feature can make opening more visible, but test it on the actual printed board and coating. The goal is a reasonable store check, not an absolute security guarantee. Do not cover warnings, product identifiers or artwork needed by buyers.
During factory testing and shipment preparation, use define visible opening evidence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Keep legitimate setup practical
Make the approved opening sequence clear for consumers and store staff.
Aggressive ties and multiple hidden tapes can damage the toy or frustrate a buyer after purchase. Ask an unfamiliar user to open the box with normal household tools and observe whether they cut near the controller wire or battery lead. Provide a simple instruction when the opening path is not obvious. A secure pack should still support safe, understandable first use.
During factory testing and shipment preparation, use keep legitimate setup practical as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Protect the demonstration unit
Decide whether shelf samples and sealed sellable units use the same pack design.
A retailer may open one unit for demonstration and leave the others sealed. Mark the demo clearly so it is not accidentally returned to sale as new stock. If the product must remain visible through a window, verify that the vehicle cannot be removed without obvious damage and that accessory retention survives normal handling.
During factory testing and shipment preparation, use protect the demonstration unit as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Test distribution effects
Check whether the added seal or closure survives packing, freight and retail handling.
A seal that breaks in a master carton can generate false tamper concerns at receiving. Test the finished pack under the relevant route and inspect at both carton and retail-unit levels. Consider abrasion against neighboring boxes and temperature effects on adhesive. A design change to improve shelf security should not silently weaken transit protection.
During factory testing and shipment preparation, use test distribution effects as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Make store inspection quick
Create a short checklist for intact seals, accessory presence, barcode and pack condition.
Store staff will not inspect a complex hidden mechanism on every sale. Put the evidence point where it can be seen during normal stocking and returns processing. If a seal is broken, define whether the unit is quarantined, inspected or discounted under retailer policy. Keep this operational decision separate from product safety investigation.
During factory testing and shipment preparation, use make store inspection quick as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Review returns by cause
Compare missing-item reports, damaged seals and first-use complaints after the packaging change.
A lower theft rate is not useful if customers increasingly damage battery doors while opening. Analyze observations by SKU and packaging revision. If factory packing checks show complete units but customers receive missing accessories, review both the shelf exposure and the return process before assigning blame. Use the findings to refine the next print run.
During factory testing and shipment preparation, use review returns by cause as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A retailer finds several RC car boxes on the shelf with the vehicle present but the charging cable missing. The brand first checks factory pack-out records and returns data before assuming theft. A physical store review shows that the open window lets a person reach the accessory compartment without visibly damaging the box. The packaging team moves the cable behind an inner flap and adds a seal that leaves clear evidence when opened. A store employee then tests whether the package can be checked quickly at receiving and whether a legitimate customer can open it safely at home. The revised box is shipped through a representative distribution route to ensure the seal does not fail under normal friction. The retailer tracks missing-item reports by packaging version after launch. The solution is judged by complete customer sets and a practical store process, not by a claim that the box is impossible to tamper with.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISTA transport packaging test procedures: Official overview of package integrity and distribution simulation procedures.
Photography plan for this article
Article hero image — After the opening section
Image title: Tamper-Evident RC Toy Packaging for Retail — RC toy sourcing overview
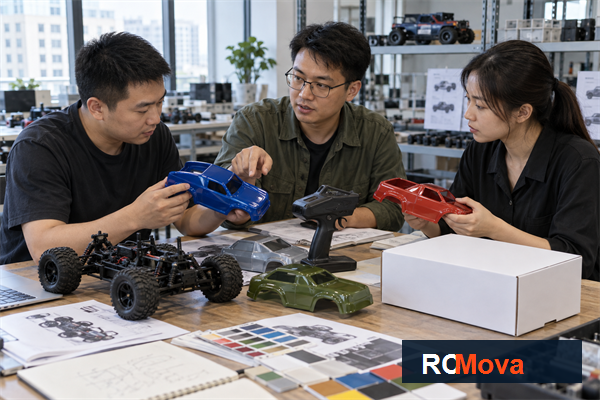
Caption: An OEM or ODM discussion is clearer when product samples, controllers and packaging direction are reviewed together. Article focus: rc toy tamper evident packaging.
ALT text: Asian toy engineers reviewing RC vehicle body shells and packaging samples in Shenzhen; rc toy tamper evident packaging buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for Tamper-Evident RC Toy Packaging for Retail, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
Image title: Tamper-Evident RC Toy Packaging for Retail — RC toy quality and shipment check
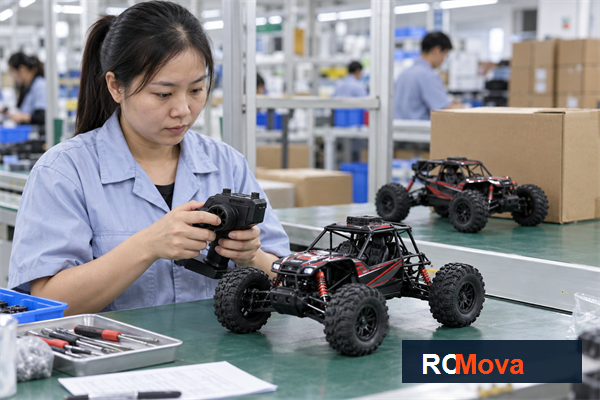
Caption: Production review for rc toy tamper evident packaging before the export handoff.
ALT text: Asian quality team reviewing rc toy tamper evident packaging with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy tamper evident packaging against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about identify the missing-item risk?
List the controller, battery pack, charging cable, manual and detachable accessories in the retail box. A vehicle may remain on display while a small charger disappears. Review which items can be reached through windows or gaps and which are hidden in a secondary compartment. Use retailer shrink and return data if available, but do not assume every missing accessory is theft; packing errors can look the same at the customer-service desk.
How should buyers verify protect the demonstration unit?
Decide whether shelf samples and sealed sellable units use the same pack design. A retailer may open one unit for demonstration and leave the others sealed. Mark the demo clearly so it is not accidentally returned to sale as new stock. If the product must remain visible through a window, verify that the vehicle cannot be removed without obvious damage and that accessory retention survives normal handling.
What should be confirmed before shipment?
Compare missing-item reports, damaged seals and first-use complaints after the packaging change. A lower theft rate is not useful if customers increasingly damage battery doors while opening. Analyze observations by SKU and packaging revision. If factory packing checks show complete units but customers receive missing accessories, review both the shelf exposure and the return process before assigning blame. Use the findings to refine the next print run.
Conclusion: turn the decision into a working plan
Map what can be removed at the shelf, select visible opening evidence and test the pack with both store staff and shoppers before bulk production. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements