Supplier Capacity
RC Toy Supplier Capacity and Line Loading: Buyer Guide
Factory capacity is not one headline number. For an RC toy order, usable capacity depends on the approved model, mold access, component readiness, assembly content, test time and packing format during the requested production window.
Direct answer: Verify the specific production route and its constraints, then connect reserved capacity to dated material, assembly, testing, packing and shipment milestones. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Importers need to verify whether a supplier can reserve realistic people, equipment and component capacity for the required delivery window. A quoted lead time can look achievable while molds, assembly lines or key electronics are already committed to other orders.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see How Do I Evaluate a Supplier, MOQ, Lead Time, Quality Control, and Delivery Plan for Remote Control Toys?, How Do I Evaluate a Supplier, MOQ, Lead Time, Quality Control, and Delivery Plan for RC Toys?, RC Toy Cartons and Container Loading: Export Planning Guide.
1. Define the exact order configuration
Capacity should be reviewed for the approved SKU mix, not for a generic RC toy category.
List each model, color, controller, battery arrangement, retail pack and destination version. A mixed order may share a chassis but require different body molding, artwork or manuals. Ask the supplier to translate the purchase quantity into units by production route. This creates a usable baseline for line loading and prevents one broad factory number from hiding a bottleneck that applies only to the selected configuration.
During factory testing and shipment preparation, use define the exact order configuration as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Map the production route
Identify every internal and external step from material release to finished-carton inspection.
A route may include injection molding, paint or printing, PCB preparation, subassembly, final assembly, radio pairing, charging checks and packing. Record which processes are performed on site and which depend on external providers. For outsourced steps, establish the named provider, planned handoff and incoming verification rather than assuming that the factory controls unlimited subcontract capacity.
During factory testing and shipment preparation, use map the production route as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Find the true constraint
Ask which mold, component, fixture, technician or packing operation limits output during the requested weeks.
The slowest resource determines practical throughput. A supplier may assemble quickly but have only one stable test fixture, one shared body mold or a battery delivery that arrives late. Compare rated cycle time with recent stable output for a similar configuration, while recognizing that another product is not perfect proof. The goal is to expose the planning assumption that needs the closest follow-up.
During factory testing and shipment preparation, use find the true constraint as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Separate theoretical and committed capacity
A maximum line rate is different from capacity reserved for the buyer’s purchase order.
Request a dated loading plan that shows other confirmed commitments only at an appropriate summary level. The factory does not need to disclose confidential customer details, but it should explain how the requested slot is protected. Note planned overtime, additional lines or temporary labor as risks to validate, not automatic capacity. A commitment should include the condition under which the reservation can change.
During factory testing and shipment preparation, use separate theoretical and committed capacity as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Connect materials to the schedule
Production capacity cannot be used when motors, PCBs, batteries, packaging or accessories are unavailable.
Review long-lead components and buyer-dependent approvals before confirming the start date. A packaging delay can block completed vehicles, while an unapproved battery substitution can stop testing and compliance review. Use a material readiness checkpoint with quantities and expected arrival dates. If partial material is planned, define which SKUs can run without creating mixed-version inventory.
During factory testing and shipment preparation, use connect materials to the schedule as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Set evidence-based milestones
Track outputs that the buyer can verify rather than a percentage-complete estimate.
Useful milestones include approved artwork released, major materials received, first mass-production units checked, assembly quantity completed, cartons packed and inspection available. Ask for dated records or representative photographs tied to the order. Progress should be reported by SKU and stage so a late color or accessory is visible before the entire order reaches the promised ship date.
During factory testing and shipment preparation, use set evidence-based milestones as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Prepare a capacity recovery plan
Agree how the supplier will respond if output falls behind the dated plan.
Name the escalation contact, decision deadline and acceptable recovery options. Adding labor may help packing but not a mold bottleneck; switching a component may require buyer approval and renewed testing. Protect product quality by keeping required checks in the recovery schedule. At shipment inspection, reconcile finished quantities with the final plan and record any balance that moves to a later dispatch.
During factory testing and shipment preparation, use prepare a capacity recovery plan as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
Imagine a distributor ordering three RC truck colors for a holiday promotion. The supplier says monthly capacity is sufficient, but the figure combines several workshops and assumes all electronics are already available. The buyer asks for a model-level route showing molding, decoration, assembly, function testing and packing. That review reveals that the body mold can support the quantity, while the shared controller test station is booked by another project. The parties move one color to a later packing wave, reserve the test fixture by date and define a weekly output report. This illustrative buyer scenario shows why a credible capacity answer identifies the constraint and recovery plan instead of presenting only a theoretical monthly total.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
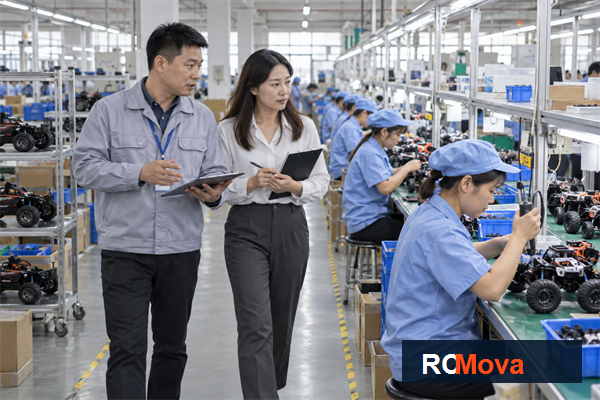
Article hero image — After the opening section
Image title: RC Toy Supplier Capacity and Line Loading: Buyer Guide — RC toy sourcing overview
Caption: A factory audit is more useful when buyers follow the product flow from assembly through packing. Article focus: rc toy supplier capacity.
ALT text: Asian buyer and factory supervisor reviewing an RC toy production line in Shenzhen; rc toy supplier capacity buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Supplier Capacity and Line Loading: Buyer Guide, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
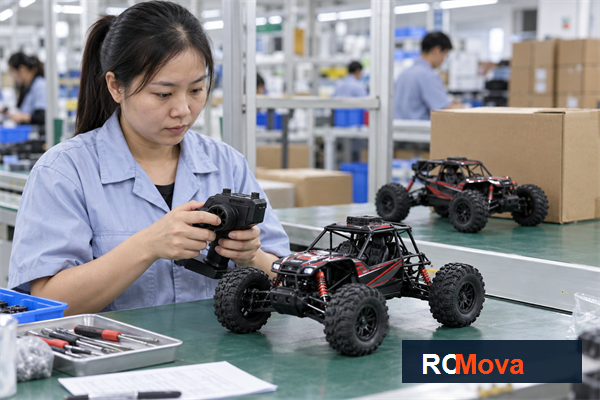
Image title: RC Toy Supplier Capacity and Line Loading: Buyer Guide — RC toy quality and shipment check
Caption: Production review for rc toy supplier capacity before the export handoff.
ALT text: Asian quality team reviewing rc toy supplier capacity with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy supplier capacity against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define the exact order configuration?
Capacity should be reviewed for the approved SKU mix, not for a generic RC toy category. List each model, color, controller, battery arrangement, retail pack and destination version. A mixed order may share a chassis but require different body molding, artwork or manuals. Ask the supplier to translate the purchase quantity into units by production route. This creates a usable baseline for line loading and prevents one broad factory number from hiding a bottleneck that applies only to the selected configuration.
How should buyers verify separate theoretical and committed capacity?
A maximum line rate is different from capacity reserved for the buyer’s purchase order. Request a dated loading plan that shows other confirmed commitments only at an appropriate summary level. The factory does not need to disclose confidential customer details, but it should explain how the requested slot is protected. Note planned overtime, additional lines or temporary labor as risks to validate, not automatic capacity. A commitment should include the condition under which the reservation can change.
What should be confirmed before shipment?
Agree how the supplier will respond if output falls behind the dated plan. Name the escalation contact, decision deadline and acceptable recovery options. Adding labor may help packing but not a mold bottleneck; switching a component may require buyer approval and renewed testing. Protect product quality by keeping required checks in the recovery schedule. At shipment inspection, reconcile finished quantities with the final plan and record any balance that moves to a later dispatch.
Conclusion: turn the decision into a working plan
Verify the specific production route and its constraints, then connect reserved capacity to dated material, assembly, testing, packing and shipment milestones. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements