Responsible Sourcing
RC Toy Supplier Social Responsibility Review
Responsible sourcing is an ongoing due-diligence process rather than a badge. RC toy buyers should connect supplier policy, risk assessment, worker information, corrective action and subcontractor visibility to their own requirements.
Direct answer: Define the buyer code, prioritize the most serious risks, use qualified assessments where appropriate and track corrective actions without making unsupported ethical claims. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Retailers and importers need proportionate evidence that supplier labor and management practices align with their policies and customer expectations. A certificate snapshot may not reveal recruitment, working-hours, grievance or subcontracting risks throughout a changing supply chain.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see How Do I Evaluate a Supplier, MOQ, Lead Time, Quality Control, and Delivery Plan for Remote Control Toys?, How Do I Evaluate a Supplier, MOQ, Lead Time, Quality Control, and Delivery Plan for RC Toys?, RC Toy Supplier Communication and Order Tracking: B2B Guide.
1. Set the buyer standard
Provide the supplier code, prohibited practices, documentation expectations and escalation route before nomination.
Requirements may cover labor, health and safety, environment, ethics and management systems. Make them proportionate to the business and applicable law. Avoid presenting a private policy as a government certification.
During factory testing and shipment preparation, use set the buyer standard as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Map the production chain
Identify the factory and important external processes used for the selected RC toy program.
Injection molding, printing, electronics and packing may occur at different sites. Prioritize visibility where risks are most likely or severe. Respect legitimate confidentiality while requiring enough information to evaluate the actual relationship.
During factory testing and shipment preparation, use map the production chain as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Review management evidence
Look for policies, responsible owners, training, worker records, grievance channels and follow-up practices.
Documents should be consistent with interviews and site conditions when a qualified assessment is conducted. One tidy file does not prove implementation. The goal is to understand whether issues can be identified, reported and corrected.
During factory testing and shipment preparation, use review management evidence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Consider worker voice
Use appropriate confidential methods to understand whether workers know their rights, hours, pay and grievance options.
Worker interviews require trained assessors and protection from retaliation. Buyers should not run informal questioning that exposes individuals. Use the findings to identify system improvements, not to collect promotional quotes.
During factory testing and shipment preparation, use consider worker voice as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Evaluate high-risk periods
Review recruitment, overtime, temporary labor and subcontracting during peak production or schedule recovery.
Practices can change when holiday orders compress the plan. Capacity reviews and purchasing behavior should not create unrealistic deadlines that undermine the buyer’s own standards. Include responsible lead-time decisions in corrective planning.
During factory testing and shipment preparation, use evaluate high-risk periods as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Manage corrective actions
Prioritize serious impacts, assign owners and dates, and verify closure through suitable evidence.
A finding should not be hidden by switching suppliers without considering consequences for workers. Escalation and remediation need qualified judgment. Track recurring issues and adjust order planning or supplier status where progress is inadequate.
During factory testing and shipment preparation, use manage corrective actions as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Communicate claims carefully
Describe the due-diligence process accurately and avoid broad claims that all products or suppliers are “ethical.”
Marketing statements should match the scope, date and limitations of evidence. Keep internal records available for customer questions. Update assessments when sites, processes or risk conditions change.
During factory testing and shipment preparation, use communicate claims carefully as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A retailer asks an RC toy supplier for a social-audit certificate shortly before order release. The certificate is current, but the selected product uses an off-site decoration provider that is not included in the assessment scope. In this illustrative scenario, the buyer maps the actual production route, reviews risk and asks the supplier to include the external process in its due-diligence plan. The decision is based on scope and corrective action rather than the presence of a logo on one report.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see OECD due diligence policy mapping: Official OECD framework for embedding responsible conduct, identifying impacts and tracking action across supply chains.
Photography plan for this article
Article hero image — After the opening section
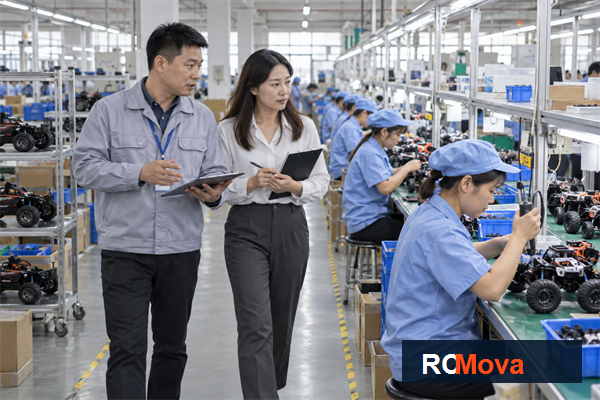
Image title: RC Toy Supplier Social Responsibility Review — RC toy sourcing overview
Caption: A factory audit is more useful when buyers follow the product flow from assembly through packing. Article focus: rc toy social compliance audit.
ALT text: Asian buyer and factory supervisor reviewing an RC toy production line in Shenzhen; rc toy social compliance audit buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Supplier Social Responsibility Review, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
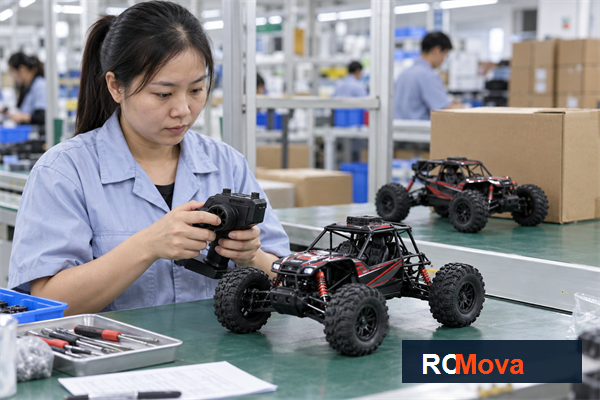
Image title: RC Toy Supplier Social Responsibility Review — RC toy quality and shipment check
Caption: Production review for rc toy social compliance audit before the export handoff.
ALT text: Asian quality team reviewing rc toy social compliance audit with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy social compliance audit against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about set the buyer standard?
Provide the supplier code, prohibited practices, documentation expectations and escalation route before nomination. Requirements may cover labor, health and safety, environment, ethics and management systems. Make them proportionate to the business and applicable law. Avoid presenting a private policy as a government certification.
How should buyers verify consider worker voice?
Use appropriate confidential methods to understand whether workers know their rights, hours, pay and grievance options. Worker interviews require trained assessors and protection from retaliation. Buyers should not run informal questioning that exposes individuals. Use the findings to identify system improvements, not to collect promotional quotes.
What should be confirmed before shipment?
Describe the due-diligence process accurately and avoid broad claims that all products or suppliers are “ethical.” Marketing statements should match the scope, date and limitations of evidence. Keep internal records available for customer questions. Update assessments when sites, processes or risk conditions change.
Conclusion: turn the decision into a working plan
Define the buyer code, prioritize the most serious risks, use qualified assessments where appropriate and track corrective actions without making unsupported ethical claims. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements